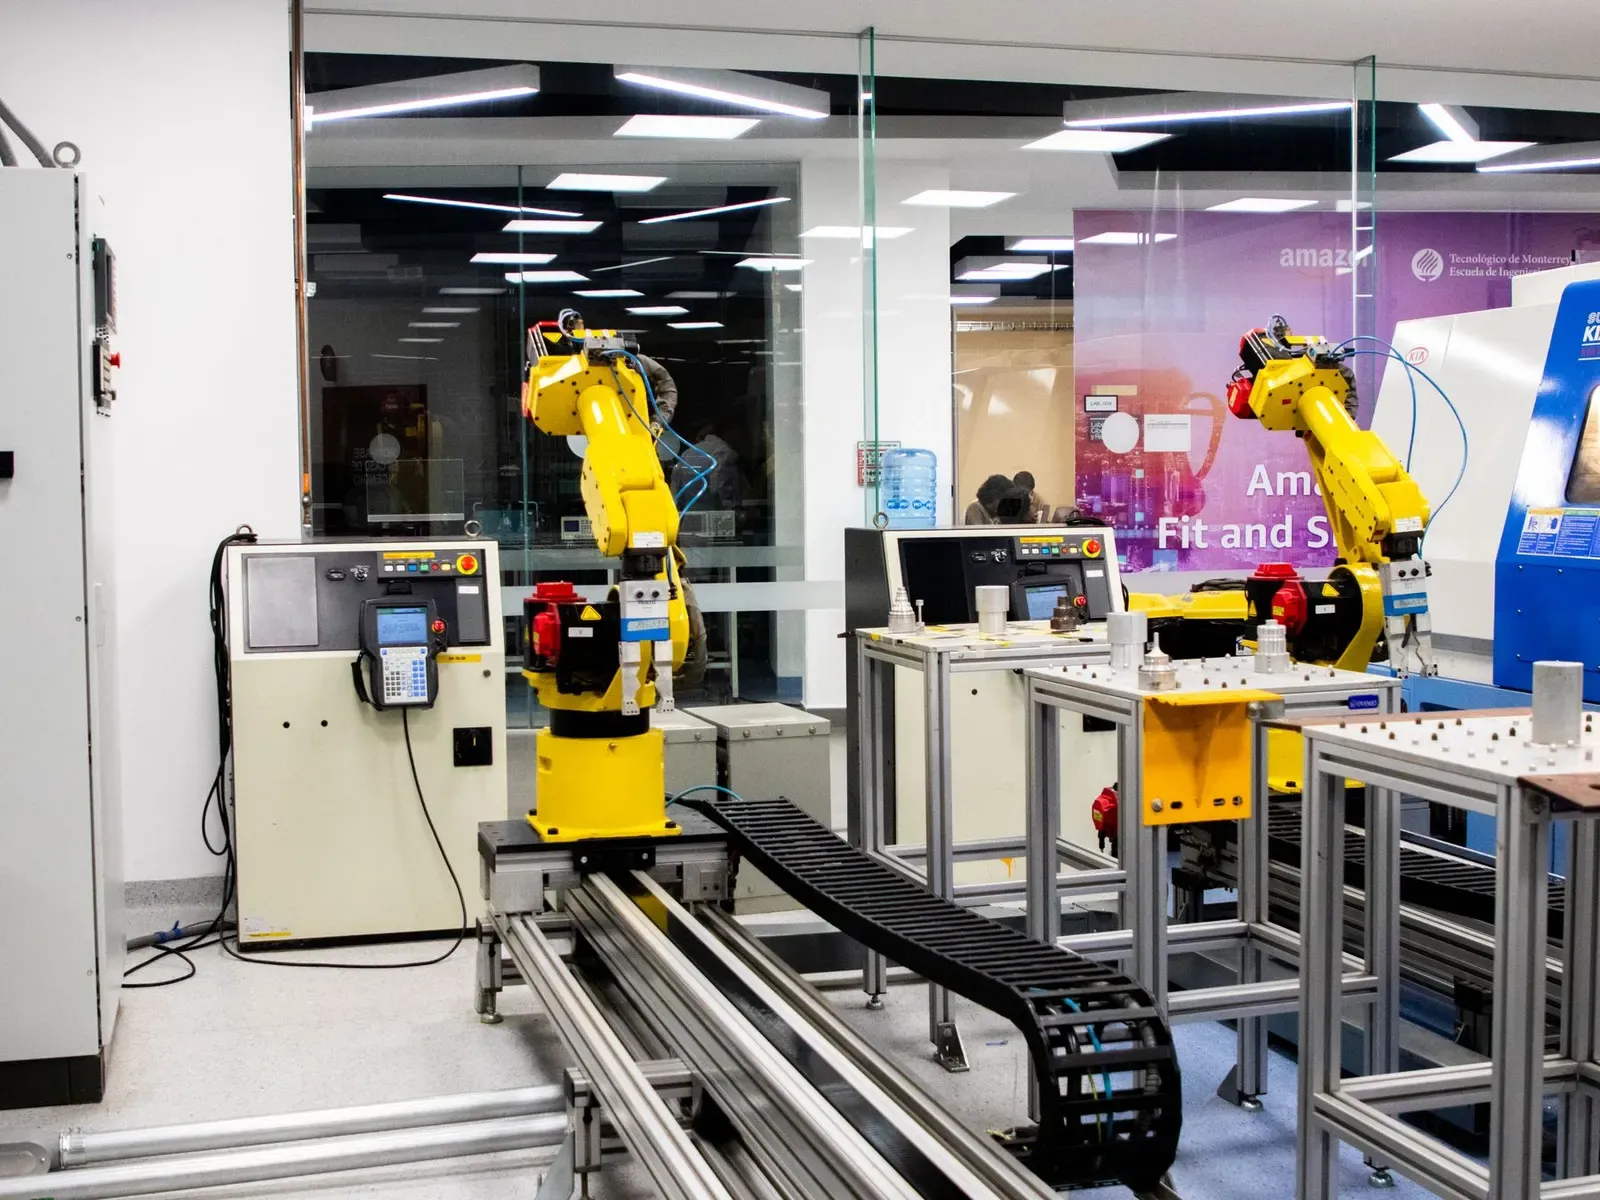
Industry 4.0 means connecting machines, sensors and business software so that production generates a steady stream of reliable data. AI integration builds on that data: it is used to spot early signs of equipment failure, catch defective products, and improve energy use and production planning. AI does not transform a factory on its own; it works when you start with good data, one specific problem and a measurable goal.
We first published this article in April 2026 and expanded it in October 2026. It now covers use cases, data prerequisites and how to start a project in more concrete terms.
What does Industry 4.0 mean?
The concept comes from Germany. According to the project page of acatech, the German academy of science and engineering, the Industrie 4.0 Working Group presented its recommendations to Chancellor Angela Merkel at Hannover Messe on 8 April 2013. The report set out the requirements for a successful transition to what it called the fourth industrial age.
In practice, Industry 4.0 is about connecting the layers of a factory. The ISA-95 standard from the International Society of Automation describes those layers like this:
| Level | What it covers | Examples |
|---|---|---|
| 0 | The physical production process | Machines, production lines |
| 1 | Sensing and manipulating the process | Sensors, valves, smart devices |
| 2 | Monitoring and supervisory control | PLCs and distributed control systems |
| 3 | Manufacturing operations management | Manufacturing execution system (MES) |
| 4 | Business planning and logistics | Enterprise resource planning (ERP) |
In an unconnected plant these layers are cut off from one another: the fact that a machine stopped stays in the operator’s logbook, and output is typed into the ERP by hand at the end of the day. The core of Industry 4.0 is data flowing between these layers automatically and securely. OPC UA is one of the standards developed for this exchange; the OPC Foundation describes it as a platform-independent architecture that runs anywhere from an embedded microcontroller to cloud infrastructure, with encryption and authentication built in.
Concrete AI use cases in manufacturing
Predictive maintenance
Predictive maintenance watches for changes in sensor data such as vibration, temperature and current to catch the early signs of a failure. The aim is to plan maintenance around the actual condition of the equipment rather than a fixed calendar or a breakdown. The model raises an alert; the maintenance team makes the call. We cover this in detail in our predictive maintenance article.
Visual quality inspection
Cameras on the line capture each product, and a model flags defects such as scratches, stains or missing parts. The practical difficulty is that defective samples are rare and varied. That is why anomaly detection methods were developed that train only on images of good products and flag anything that deviates from normal. The MVTec AD dataset, built for industrial inspection, was created to benchmark these methods: it contains more than 5,000 images across 15 categories, and its training sets contain only defect-free items. On the shop floor, products the model is unsure about go to a human inspector.
Energy optimisation
Measurement comes first. Unless energy use is tracked per line or per machine, alongside output, you cannot tell what to improve. Once the data is there, idle equipment, avoidable peak loads and differences between shifts become visible, and forecasting models help predict consumption together with the production plan. The international framework for energy management is ISO 50001; the US Department of Energy’s 50001 Ready programme breaks the standard’s Plan-Do-Check-Act cycle into seven actionable steps.
Demand and production planning
You can forecast demand from past orders, sales and seasonality, and set production plans and stock levels accordingly. Not everything is equally predictable, though. According to Hyndman and Athanasopoulos’s Forecasting: Principles and Practice, how predictable something is depends on how well we understand the factors behind it, how much data is available, how similar the future is to the past, and whether the forecast itself affects the outcome. A new product’s demand is therefore harder to forecast than an established one’s, and forecasts are best read as a range rather than a single number.
Data first: what AI needs
In an AI project, look at the data before the model. Check these before you start:
- Sensor data: collected from the right points, at the right frequency and with timestamps. Fast-changing signals need much more frequent sampling than slow ones.
- Context data: whether the machine was running, which product it was making, whether it was under maintenance. Sensor data without context leads to false alarms.
- Event records: failures, stoppages, defective products and their causes. This is how a model learns what “bad” looks like; if these records live in paper logbooks or free text, they need tidying first.
- Data quality: missing readings, sensors whose calibration drifts over time, mixed units and clock differences are problems to solve before modelling.
- Integration with existing systems: the picture is incomplete until data from PLCs, the MES and the ERP is brought together. ISA-95 specifically defines the interface between manufacturing operations (level 3) and business systems (level 4).
Connecting machines to a network also widens the attack surface; we discuss this in our article on cybersecurity in industrial networks. For collecting data from the field, see our article on IoT remote monitoring.

Where to start: one line, one goal
- Pick one problem. Start with whatever costs you most: unplanned downtime, scrap rate or the energy bill.
- Narrow the scope. Choose a single line, or even a single critical machine, rather than the whole plant.
- Measure the baseline. Before setting a target, measure the current state for a few weeks or months, for example “monthly unplanned downtime on line 3” or “scrap rate on the packaging line”. Without a baseline, you cannot measure the result.
- Collect and check the data. Add missing sensors, tidy up records and make sure the data can be trusted.
- Start simple. Rule-based thresholds or basic statistical models give you a benchmark. A more complex model only makes sense if it beats that benchmark.
- Review with operators. The team on the floor sees and interprets the alerts. Too many false alarms and trust disappears, so feed their input back into the model.
- Roll out if the result holds up. If you hit the target, take the same approach to other lines; if you don’t, learning why is a useful result too.
When projects like this involve genuine R&D, they may also qualify for funding programmes; we cover the options available in Turkey in our article on TÜBİTAK and KOSGEB funding.
Common pitfalls
- Starting with the technology: buying a platform first and then looking for a problem it fits. The right order is problem, data, method.
- Trying to transform everything at once: the bigger the scope, the more data problems pile up, the later the results and the weaker the support for the project.
- Leaving data quality for later: a model cannot be better than the data it is fed.
- Inflated expectations: AI can reduce errors and surface failures earlier, but it does not eliminate errors and it does not make the right decision on its own in every situation. The model should produce alerts and recommendations, and critical decisions should stay with people.
- Forgetting maintenance after the pilot: a new product, a replaced sensor or a different raw material changes the conditions the model learned from. Monitor its performance regularly and retrain it when needed.
Frequently asked questions
Can older machines be part of Industry 4.0?
Often, yes. If a machine’s own controller does not expose data, external vibration, current or temperature sensors and a gateway can collect it. What matters is knowing from the start which question that data is meant to answer.
How much data does AI need?
It depends on the task. Visual anomaly detection can start with images of good products only, as in the MVTec AD example. Demand forecasting needs history covering several seasons. In predictive maintenance, it is hard to validate the model’s alerts without past failure records.
Conclusion
Industry 4.0 is about data flowing continuously and securely from machines to business systems. When AI is built on that data, it can bring measurable improvements in maintenance, quality, energy and planning. The most solid start is one line, a measured baseline and a clear target.
We bring image processing, signal processing and AI modules to the shop floor in R&D software projects. If you are looking for a starting point on your production line, take a look at our AI solutions and smart city and IoT pages or get in touch, and we can look at your data and your goals together.